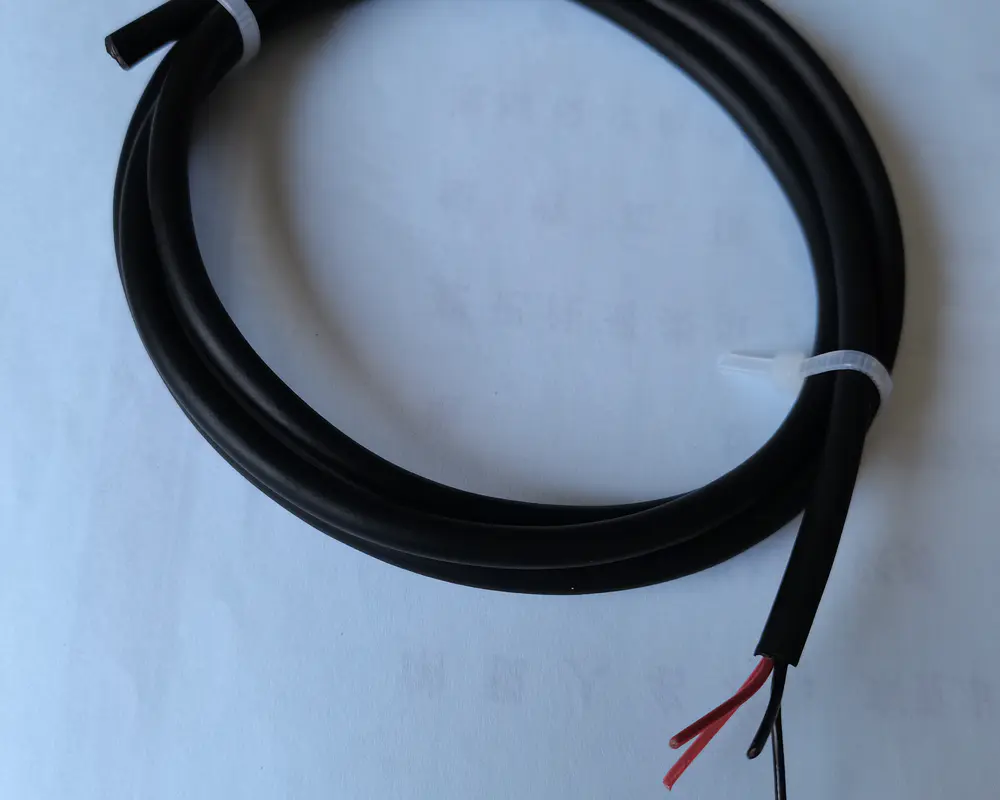
Gel water blocking involves the careful application of water-repelling gel to a cable’s shield to help stop the longitudinal migration of water. During the manufacturing process, the gel is carefully applied to fill-in gaps within the cables internal conductors. Once the final, outer jacket is applied, and having filled-in all internal gaps, the migration of water through the cable is less likely. CITCABLE recommends the use of gel water blocking technology as part of a comprehensive design including proper termination and selection of suitable connectors.


The Water Blocked Wire Cable is designed with a silicone-filled conductor core that prevents water and fluids from migrating along the conductor through capillary action. This construction helps maintain electrical performance and prevents failures caused by fluid penetration.
| Layer | Material | Function |
|---|---|---|
| Conductor | Stranded copper (0.15–10.0 mm², ASTM B-33) | Provides stable electrical conductivity and flexibility |
| Water-Blocking Core | Silicone blocking compound | Fills strand gaps and blocks fluid migration along the cable |
| Swellable Tape (optional) | Water-swellable tape or yarn | Expands on contact with water to seal the strand bundle |
| Insulation Layer | FKM / FEP / ETFE / XLPE / PVDF | Provides heat and chemical resistance |
| Shield (optional) | Tinned copper braid | Provides EMI screening and grounding for sensor circuits |
| Outer Layer | Fluoroelastomer jacket | Improves mechanical and fluid protection |
Water blocking works by removing the empty space that water needs. In a standard stranded cable, the gaps between the strands form a continuous channel. A water blocked cable fills those channels with a silicone compound, so water can wet the outside of the cable but cannot travel along the conductor to a terminal, a sensor or a control unit.
|
Without Water Blocking Water → strand gaps → terminals & equipment
Common Failures:
|
With Water Blocking Water ❚❚ blocked by silicone water-blocking core
Engineering Advantages:
|
Many water blocked cables rely on petrolatum or hot-melt filler. These soften and start to flow above roughly 90 °C — exactly the temperature range an engine or transmission harness operates in. Once the filler drains out of the core, the voids return and the barrier is gone. The silicone compound used in this cable stays in place from -50 °C to +200 °C, does not melt under overload, and keeps the 0.15–10.0 mm² ASTM B-33 copper conductor sealed at its full 600 V DC rating throughout thermal cycling.
Engineering note: water blocking protects the length of the cable, not the connector. Terminations, splices and connector interfaces still need sealing, and the cable should be bent within its rated radius so that the core and insulation are not deformed. CITCABLE recommends gel blocking as part of a complete system that includes sealed connectors and correct termination.
| Rated temperature: | -50℃ ~ 200℃ |
| Rated voltage: | 600V DC |
| Conductor: | 0.15mm2 to 10.0mm2 fully annealed stranded copper Per ASTM B-33 |
| Operating temperature range: | -40 °C to +200°C for Fluoroelastomer/ VITON/XLFE/FKM |
| -60 °C to +200°C for FEP | |
| -60 °C to +200°C for XLETFE | |
| -60 °C to +175°C for ETFE | |
| -40 °C to +150°C for PVDF | |
| -40 °C to +150°C for XLPE | |
| -40 °C to +125°C for XLPE | |
| -40 °C to +105°C for PVC |
We provide customized anti-capillary wire cable solutions tailored to your specific application requirements, ensuring optimal performance for your machinery.
| Customization Item | Options |
|---|---|
| Conductor Size | 0.35mm² - 6.0mm² |
| Insulation Material | FKM / FEP / ETFE / XLPE / PVDF |
| Voltage Rating | Customized according to requirement |
| Color | Black, Red, Blue, or Custom colors |
| Cable Length | Customized packaging / cut to length |
With advanced cable extrusion equipment and strict quality control processes, we provide customized anti-capillary wire cable solutions for industrial OEM customers. Our capabilities include:
| Test Item | Purpose |
|---|---|
| Oil Resistance Test | Verify insulation durability under continuous fluid exposure |
| High Temperature Test | Check thermal stability and prevent melting/degradation |
| Voltage Withstand Test | Ensure electrical safety and prevent breakdown |
| Flexibility Test | Evaluate mechanical performance in dynamic applications |
| Fluid Migration Test | Verify the effectiveness of the anti-capillary structure |
A:The cable is rated from -50 °C to +200 °C overall, with the final range set by the insulation: FKM, FEP and XLETFE reach +200 °C, ETFE +175 °C, PVDF and XLPE +150 °C, and PVC +105 °C. Select the insulation from the hottest point the cable will see in service, not from the average ambient temperature, and tell us the peak temperature when you request a quotation.
A:Yes. This construction is intended for cables that sit in standing water, run underwater, are exposed to constant humidity, or are installed outdoors where the jacket may be damaged and the ends left open. For pressurised or deep submersion, send us the depth and the expected hydrostatic head so we can confirm the design before production.
A:MOQ depends on conductor size, insulation material, blocking construction and total length, because a special compound and a non-standard insulation take longer to set up than a stock build. Conductor size, insulation, colour, cut length, printing and packaging can all be specified. Send the specification and your annual volume, and we will confirm MOQ, sample lead time and price in the quotation.
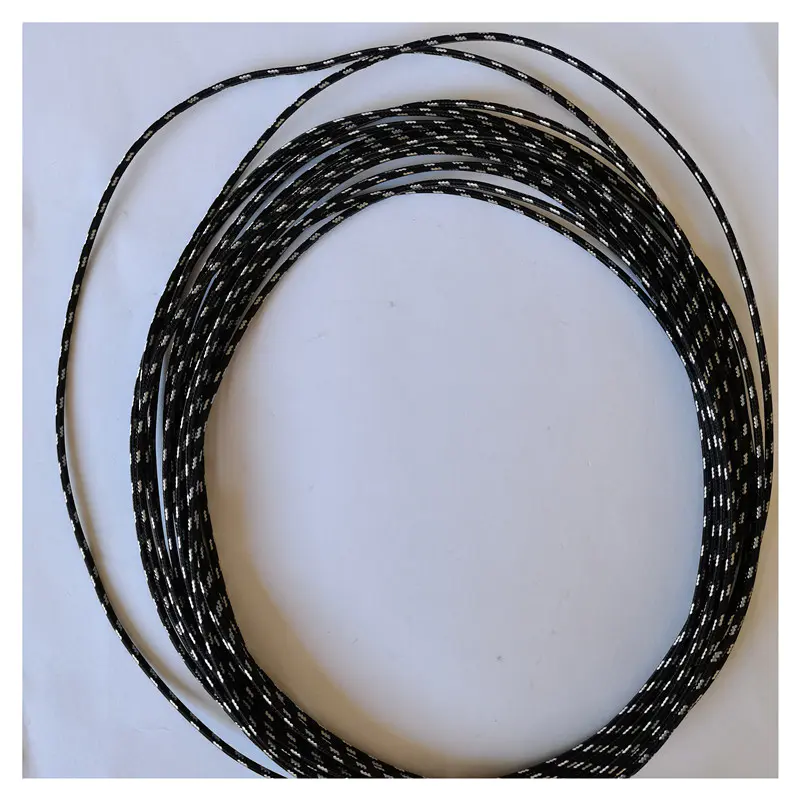
Highly Fluid Resistant Wire is a very high performance fluid blocking wire built to handle the high temperature fluid environments in engines and transmissions. It is a fluoroelastomer with impressive properties including great flexibility. it is extremely fluid resistant even at temperatures up to 230°C. It is safer in overload conditions, because it will not melt. it has a custom-engineered silicone blocked conductor to prevent moisture and other fluids to wick through the wiring system.
Details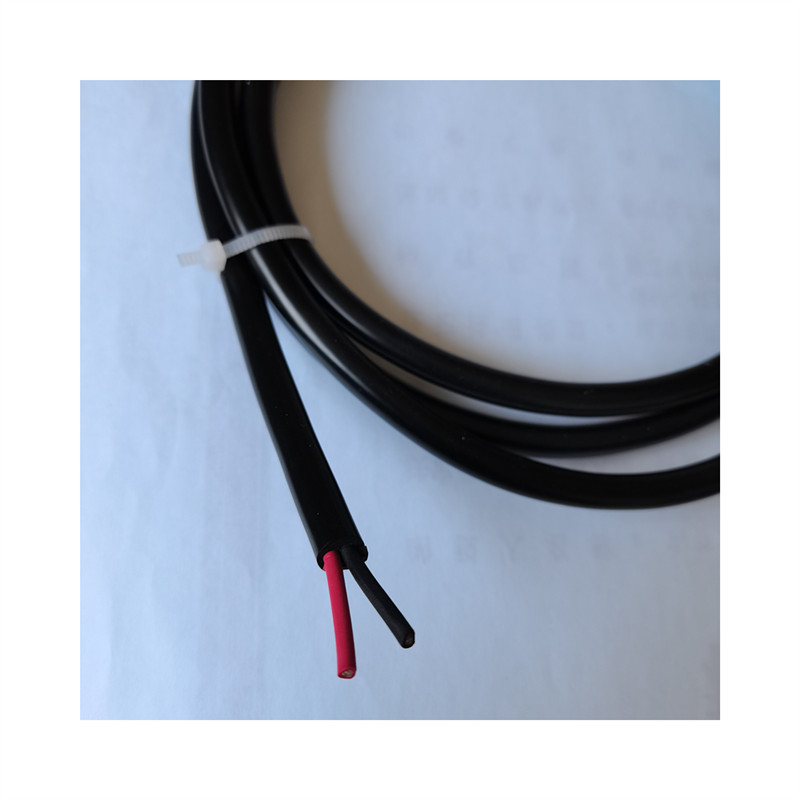
Highly Fluid Resistant Wire is a very high performance fluid blocking wire built to handle the high temperature fluid environments in engines and transmissions. It is a fluoroelastomer with impressive properties including great flexibility. it is extremely fluid resistant even at temperatures up to 230°C. It is safer in overload conditions, because it will not melt. it has a custom-engineered silicone blocked conductor to prevent moisture and other fluids to wick through the wiring cables.
Details
The Anti Capillary Wire Cable significantly enhances industrial safety by preventing fluids from traveling along the wire, which can cause short circuits or equipment malfunctions. In environments such as factories, oil rigs, and chemical plants, the cable ensures that any fluid exposure does not lead to potential electrical hazards. With its fluid-resistant properties, this cable protects the integrity of your systems, reduces the risk of downtime, and improves the overall safety of your operations.
Details
Fluid Blocking Engine/Transmission Wire is a high performance fluid blocking anti-cap wire built to handle the high temperature fluid environments in engines and transmissions.extremely fluid resistant even at temperatures up to 200°C. It is an excellent, cost effective replacement for TFE, FEP or Tefzel insulated wire,but it survives temperatures to 270°C and higher for short periods of time. It is safer in overload conditions.that will last longer than ever before, meeting 3,000 hour heat age tests. It has a life expectancy over 10,000 hours at 160°C and 20,000 hours at 150°C.CITCABLE is an anti-capillary automotive wire ideally suited in applications where heat protection, high temperature fluid resistance, fluid blocking, long life and less expensive wiring harness are required.
Details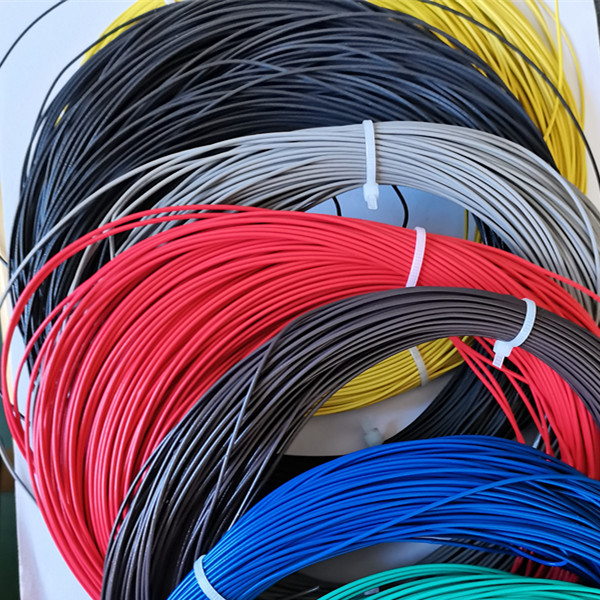
CITCABLE:200℃ Anti Capillary Wire Cable (FKM/VITON/XFLE/TEFLON) Anti Capillary Wire Cable is typically constructed using high-quality, fluid-resistant materials such as fluoropolymers, silicone, and other specialty compounds. These materials not only resist the capillary action of fluids but also provide durability, flexibility, and resistance to extreme temperatures. The combination of these materials ensures that the Anti-Capillary Wire Cable can perform reliably in harsh environments while offering long-lasting protection against fluid exposure. Fluid Compatibility 1. Engine Oil (ISO 1817. Oil No. 2)2. Engine Oil (IRM 902)3. Gasoline (Ref. Fuel C)4. Ethanol / Ref. Fuel C Mixture5. Diesel Fuel6. Battery Acid (Sp. Gr. ~ 1.26)7. Engine Coolant 50/508. E20 -40 °C to +200°C for Fluoroelastomer/ VITON/XLFE/FKM/VITON Application Greabox wiresFluid Resistant Transmission Wire200°C automatic transmission wireATF T6 wire Harness
Details
CITCABLE:200℃ Anti Capillary Wire Cable (FKM/VITON/XFLE/TEFLON,XLPE,RUBBER) Anti Capillary Wire Cable is typically constructed using high-quality, fluid-resistant materials such as fluoropolymers, silicone, and other specialty compounds. These materials not only resist the capillary action of fluids but also provide durability, flexibility, and resistance to extreme temperatures. The combination of these materials ensures that the Anti-Capillary Wire Cable can perform reliably in harsh environments while offering long-lasting protection against fluid exposure. Fluid Compatibility 1. Engine Oil (ISO 1817. Oil No. 2)2. Engine Oil (IRM 902)3. Gasoline (Ref. Fuel C)4. Ethanol / Ref. Fuel C Mixture5. Diesel Fuel6. Battery Acid (Sp. Gr. ~ 1.26)7. Engine Coolant 50/508. E20 -40 °C to +200°C for Fluoroelastomer/ VITON/XLFE/FKM/VITON Application Greabox wiresFluid Resistant Transmission Wire200°C automatic transmission wireATF T6 wire Harness
Details
Gel water blocking involves the careful application of water-repelling gel to a cable’s shield to help stop the longitudinal migration of water. During the manufacturing process, the gel is carefully applied to fill-in gaps within the cables internal conductors. Once the final, outer jacket is applied, and having filled-in all internal gaps, the migration of water through the cable is less likely. CITCABLE recommends the use of gel water blocking technology as part of a comprehensive design including proper termination and selection of suitable connectors.
Details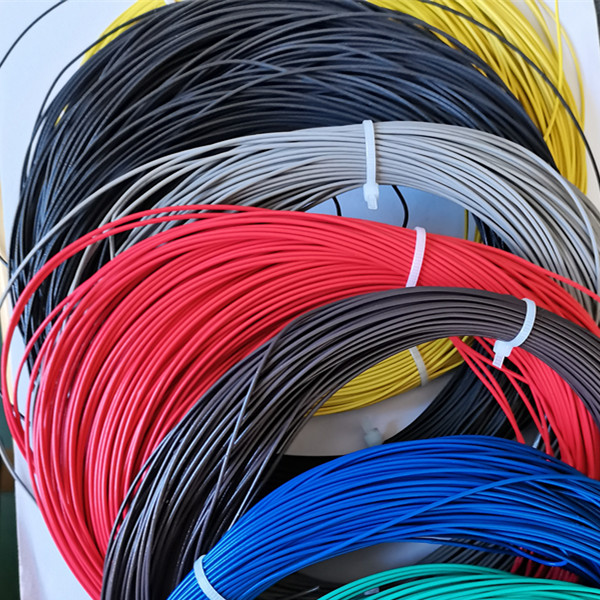
The Anti Capillary Wire Cable significantly enhances industrial safety by preventing fluids from traveling along the wire, which can cause short circuits or equipment malfunctions. In environments such as factories, oil rigs, and chemical plants, the cable ensures that any fluid exposure does not lead to potential electrical hazards. With its fluid-resistant properties, this cable protects the integrity of your systems, reduces the risk of downtime, and improves the overall safety of your operations.
Details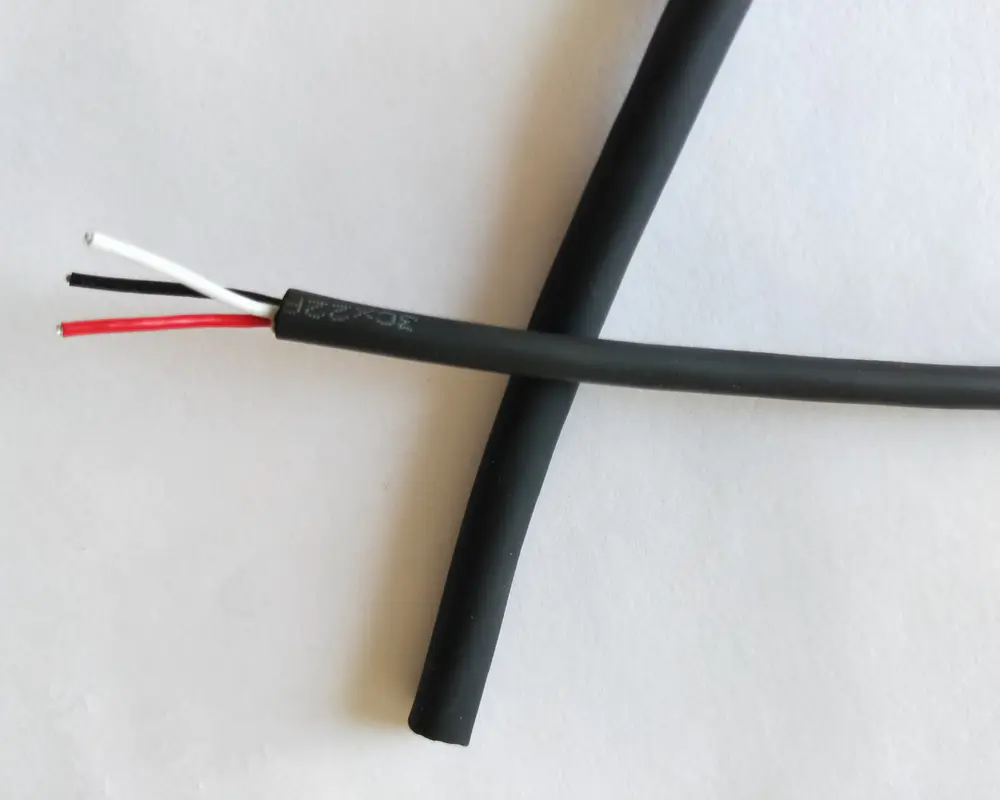
Highly Fluid Resistant Wire is a very high performance fluid blocking wire built to handle the high temperature fluid environments in engines and transmissions. It is a fluoroelastomer with impressive properties including great flexibility. it is extremely fluid resistant even at temperatures up to 230°C. It is safer in overload conditions, because it will not melt. it has a custom-engineered silicone blocked conductor to prevent moisture and other fluids to wick through the wiring system.
Details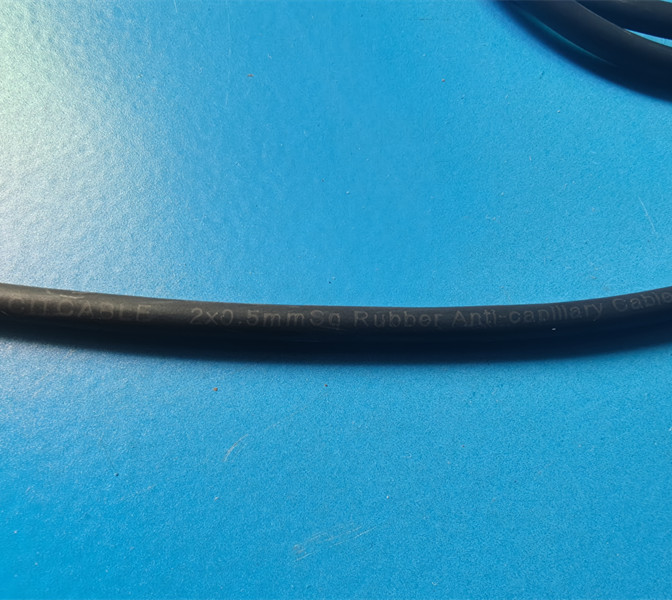
CITCABLE:20AWG 2C, 18AWG 2C, 16AWG 3C,Anti-Capillary Cable for LED Anti Capillary Wire Cable is typically constructed using high-quality, fluid-resistant materials such as fluoropolymers, silicone, and other specialty compounds. These materials not only resist the capillary action of fluids but also provide durability, flexibility, and resistance to extreme temperatures. The combination of these materials ensures that the Anti-Capillary Wire Cable can perform reliably in harsh environments while offering long-lasting protection against fluid exposure.Anti-Capillary /Fluid Compatibility 1. Engine Oil (ISO 1817. Oil No. 2)2. Engine Oil (IRM 902)3. Gasoline (Ref. Fuel C)4. Ethanol / Ref. Fuel C Mixture5. Diesel Fuel6. Battery Acid (Sp. Gr. ~ 1.26)7. Engine Coolant 50/508. E20 Application Greabox wiresFluid Resistant Transmission Wire200°C automatic transmission wireATF T6 wire Harness Anti capillary Cable for LED
Details
Fluid Blocking Engine/Transmission Wire is a high performance fluid blocking anti-cap wire built to handle the high temperature fluid environments in engines and transmissions.extremely fluid resistant even at temperatures up to 200°C.
Details3F, C Build, NO.10, MinChang Road, Nance, HuMen DongGuan City,GuangDong.China.
 IPv6 network supported